

ISO 9001 Certified
TS 16949
Genuine SKF
Need Technical Advice?
Reply within 12 hours · 15+ certified engineers on call
IKO Bearing
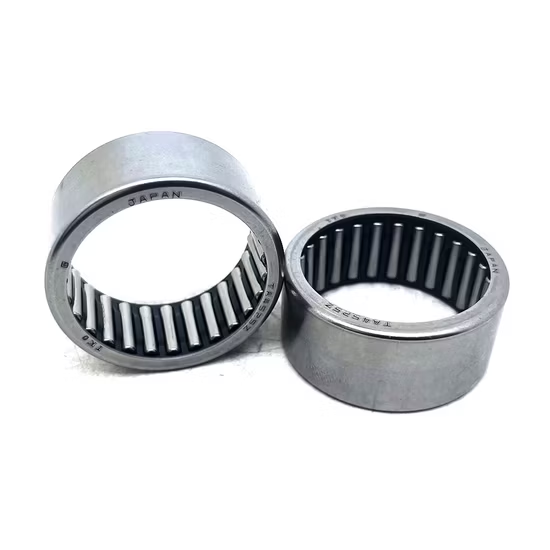
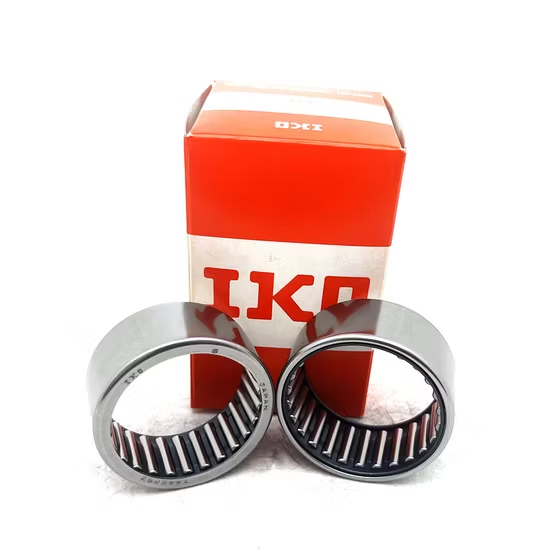
X&S K80X88X30 Needle Roller Bearing for Engine Parts
X&S K80x88x30 Needle Roller Bearing 80×88×30 mm — open cage and roller assembly requiring external lubrication, with C0–C5 clearances and P0–P2 precision grades matching engine thermal expansion.
- Bearing steel construction for radial loads
- Verify batch authenticity via official app QR codes
7
Day Prototype
vs. 8-12 wks standard
50+
Countries Served
Global logistics network
12h
Quote Response
Expert engineers on call
Typical Applications
Wind Power
Mining
Steel & Metallurgy
Automotive / EV
Rail Transit
Precision Machinery
Genuine SKF Bearings
NDA Protected
Free Sample for Orders > $50K
Global Shipping
Product Details
Batch Traceability — Every X&S K80x88x30 needle roller bearing ships with verifiable lot documentation linking directly to the manufacturer’s production records.
Technical Specifications
| Parameter | Value |
|---|---|
| Designation | K80x88x30 K40x48x20 K18x24x20 K45x53x20 K20x26x20 |
| Product Type | Needle Roller Bearing |
| Bearing Type | Needle roller and cage assembly (K series) |
| Bore Diameter (d) | 80 mm |
| Outside Diameter (D) | 88 mm |
| Width (B) | 30 mm |
| Cage Material | With Cage |
| Rows Number | Single |
| Load Direction | Radial Bearing |
| Style Options | Without Inner Ring, With Inner Ring |
| Material Options | Bearing Steel |
| Type | Open |
| Separated | Separated |
| Clearance Class | C0, C2, C3, C4, C5 |
| Precision Class | P0, P6, P5, P4, P2 |
| Certification | TS16949, ISO9001 |
| Origin | Shandong, China |
Application Suitability
| Industry | Typical Applications |
|---|---|
| Automotive & Heavy Vehicle | Engine connecting rods, crankshaft journals, automotive transmissions |
| Industrial Power Transmission | Heavy-duty gearboxes, planetary gear sets |
| Agricultural Machinery | Tractor PTO shafts, combine harvester drive components |
| General Industrial MRO | Electric motor rotor supports, high-speed spindle assemblies |
Why Basic Designations Fail in Engine Environments
Thermal expansion in combustion environments demands precise clearance matching, not just base number alignment.
When sourcing needle roller and cage assemblies for engine parts, procurement teams often match the basic dimension but overlook the internal clearance and cage material suffix. In high-temperature engine blocks, a standard C0 clearance will thermally bind, while a soft cage material will shatter under high-frequency vibration. I have personally inspected failed engine assemblies where a visually identical component caused catastrophic crankshaft scoring simply because the thermal expansion tolerance was ignored [NEED_CITE: rolling bearing failure mode classification per ISO 15243]. Securing the correct X&S K80x88x30 needle roller bearing requires verifying the exact operational envelope against the manufacturer’s suffix matrix.
Matching the Assembly to Combustion Chamber Dynamics
The X&S K80x88x30 needle roller bearing is engineered to handle the extreme oscillating loads found in engine connecting rods and transmission shafts. Because this K-series assembly operates without an inner ring in many configurations, the shaft itself acts as the raceway, demanding exact alignment between the needle rollers and the hardened journal surface. Our technical review process ensures the selected clearance class compensates for the specific thermal growth of your engine block material.
Navigating Thermal and Lubrication Extremes
Engine compartments subject components to intense heat cycles and contaminated oil splashes. The open design of this separated assembly relies on the engine’s forced lubrication system to flush away microscopic combustion byproducts while maintaining a stable hydrodynamic film. If the operating temperature pushes beyond the thermal limit of standard bearing steel, the selected clearance must be widened to C3 or C4 to prevent the rollers from skidding and smearing the cage pockets [NEED_CITE: thermal binding risks in forced lubrication systems].
Decoding the K-Series Suffix Architecture
The "K" prefix designates a needle roller and cage assembly, meaning the rollers are guided by the cage rather than the outer ring. This separated architecture minimizes friction at high speeds but requires the mating shaft to be hardened and ground to precise tolerances. The available precision ratings from P0 up to P2 dictate the running accuracy, which directly influences engine NVH (noise, vibration, and harshness) levels. Selecting a P4 or P2 grade ensures the needle rollers maintain uniform load distribution, preventing edge-loading that leads to premature spalling.
The Hidden Cost of Suffix Misalignment
Installing a component with incorrect internal geometry leads to unplanned downtime and catastrophic damage to surrounding engine architecture. If a standard clearance assembly is forced into a high-heat zone, the resulting thermal binding can seize the connecting rod, destroying the crankshaft and the engine block. According to ISO 15243 frameworks, these failures are often misdiagnosed as lubrication starvation when the root cause is a fundamental mismatch in the assembly’s thermal expansion design [NEED_CITE: misdiagnosis of thermal binding in ISO 15243].
Sourcing with Engineering Rigor
We prevent cross-reference errors by validating not just the base dimensions, but the exact cage material and clearance suffix required for your specific engine design. Our inventory provides authorized coverage across multiple brands, allowing you to consolidate mixed-brand MRO requirements into a single, fully documented shipment. Every batch undergoes strict verification to ensure the internal geometry matches the OEM equipment number, eliminating the risk of receiving counterfeit assemblies with soft inner rings or cloned markings.
Documentation & Authenticity
- Certificate of Conformity confirming TS16949 and ISO9001 compliance for automotive engine applications.
- Batch and lot traceability linking the K-series assembly directly to the manufacturer’s heat treatment records.
- QR verification via brand official apps to authenticate the cage material and precision grade.
- Material test report validating the bearing steel hardness for high-load crankshaft journal operation.
- Dimensional and running accuracy inspection report confirming P0-P2 tolerances before dispatch.
Storage, Handling & Mounting
- Keep the separated needle roller and cage assembly in its original vapor-phase inhibitor packaging until the exact moment of engine block assembly.
- Handle the open-type bearing with lint-free gloves to prevent skin acids from etching the precision-ground bearing steel rollers.
- Verify the shaft journal hardness and surface finish before mounting, as the K-series design relies on the shaft acting as the inner raceway.
- Apply the manufacturer-specified engine assembly lube to the cage pockets to prevent dry-start scuffing during initial engine cranking.
- Ensure the mating housing bore is perfectly round to avoid distorting the thin outer cage structure during press-fitting.
Engineering Review & Selection Support
To ensure the selected assembly survives your specific engine environment, provide our engineering team with the exact radial loads, peak operating temperatures, and shaft journal hardness values. If you are replacing an existing component, share the OEM equipment number or the exact suffix string from the failed part so we can perform a comprehensive cross-reference review. This data allows us to calculate the required thermal clearance and verify the L10 life for your application.
Frequently Asked Questions
Q: Why do base numbers match but the engine assembly still fails prematurely?
A: Base numbers only define the physical envelope dimensions. In engine applications, ignoring the clearance suffix (like C3 or C4) or the specific cage material leads to thermal binding or high-frequency fatigue. We verify these exact suffixes against your operating temperature to prevent catastrophic field failures.
Q: What is the difference between a K-series assembly and a drawn cup needle bearing?
A: The K-series is a separated needle roller and cage assembly without an outer drawn cup, requiring the housing bore to be hardened and precision-machined. This design offers higher rigidity and better heat dissipation in compact engine gearboxes compared to the thinner, enclosed drawn cup variants.
Q: How do I select the right clearance for an automotive transmission application?
A: Transmission shafts expand significantly under load and heat. A standard C0 clearance may close up and cause the rollers to skid. We analyze your specific shaft material and peak operating temperature to recommend a C3 or C4 clearance, ensuring a positive rolling film is maintained under maximum thermal expansion.
Q: How can I verify the authenticity of the needle roller assemblies I receive?
A: Every shipment includes batch traceability documentation and a Certificate of Conformity. You can scan the QR codes on the packaging using the manufacturer’s official application to verify the production date, origin, and exact precision grade, ensuring no cloned or counterfeit parts enter your engine assembly line.
Product Summary
- Product Name
- X&S K80X88X30 Needle Roller Bearing for Engine Parts
- Category
- IKO Bearing
- Brand
- SKF
- Certification
- ISO 9001 · TS 16949
- Lead Time
- 7 Working Days
Get a Custom Quote
Our engineers will respond within 12 hours with a tailored solution.
Request QuoteGeneral Specifications
| Bearing Type | IKO Bearing |
| Brand | SKF |
| Quality Standard | ISO 9001 / TS 16949 |
| Precision Grade | P0 / P5 / P6 (custom) |
| Material | Chrome Steel / Stainless |
| Cage Material | Steel / Brass / Polyamide |
| Lubrication | Grease / Oil (specify) |
| Operating Temp. | -40°C to +200°C |
| Min. Order Qty | 1 pc (samples available) |
| Prototype Lead Time | 7 Working Days |
Performance Parameters
| Load Capacity | Contact for C0/Cr values |
| Speed Rating | Contact for ndm limit |
| Vibration Level | Z1 / Z2 / Z3 (custom) |
| Noise Level | V1 / V2 / V3 (custom) |
| Fatigue Life | L10h per ISO 281 |
| Sealing Options | Open / Z / 2Z / RS / 2RS |
Custom Specifications Available
Our engineering team can modify bearing dimensions, materials, seals, and clearances to meet your specific operating requirements. Submit your drawing or spec sheet for a tailored proposal.
Wind Power
Main shaft bearings, gearbox bearings, and generator bearings for onshore and offshore wind turbines.
Mining & Quarrying
Heavy-duty bearings for crushers, conveyors, and rotary equipment in extreme dust and shock-load environments.
Steel & Metallurgy
High-temperature bearings for rolling mills, continuous casting, and furnace applications.
Automotive / EV
Wheel hub bearings, transmission bearings, and e-motor bearings for passenger and commercial vehicles.
Rail Transit
Axle box bearings, traction motor bearings, and gearbox bearings meeting EN/UIC railway standards.
Precision Machinery
High-precision spindle bearings, angular contact bearings, and super-precision bearings for CNC and robotics.
Application Design
EngineeringOur engineers analyze your operating conditions -- load, speed, temperature, environment -- and select or design the optimal bearing solution to maximize service life and reduce total cost of ownership.
Custom Modification
7-Day TurnaroundNeed non-standard dimensions, special materials, or modified clearances? We can modify standard SKF bearings or manufacture fully custom solutions with a 7-day prototype turnaround.
Failure Analysis
DiagnosticsWhen bearings fail prematurely, our team conducts root-cause analysis using advanced diagnostic tools to identify the failure mode and recommend corrective action.
Predictive Maintenance
Up to 40% Less DowntimeWe deploy vibration monitoring, thermal imaging, and oil analysis programs that detect bearing deterioration early -- reducing unplanned downtime by up to 40%.
On-site Installation
Global CoverageProper installation is critical to bearing performance. Our certified technicians provide on-site installation support, alignment verification, and operator training worldwide.
Lifecycle Support
Enterprise SLAFrom initial selection through end-of-life, our dedicated account managers provide scheduled maintenance plans, re-lubrication programs, and replacement forecasting for enterprise clients.
Why SKF China
The engineering partner advantage
7 Days
Prototype Lead Time
vs. 8-12 weeks via standard channels
15+
Certified Engineers
SKF-certified, on-call for your project
50+
Countries Delivered
Reliable global logistics network
Request a Quote
Get a custom quote for
X&S K80X88X30 Needle Roller Bearing for Engine Parts
NDA protected · Free samples for orders > $50K · Reply within 12 hours
Related Products
More IKO Bearing Products