Angular Contact Ball Bearing
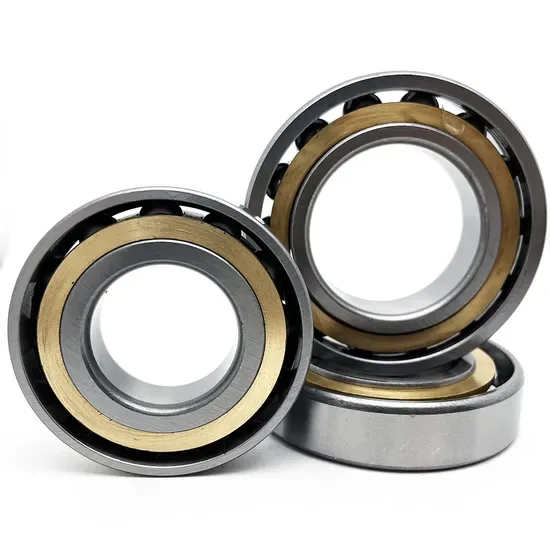
X&S 7006 7008CTYNSP5 7009AC Angular Contact Ball Bearing — 15° (C) and 25° (AC) contact angle variants with P5 precision class for machine tool spindle applications.
Every shipment includes full documentation with material test reports and dimensional inspection records for complete batch traceability.
Official App QR Verification — Every X&S 7006 7008CTYNSP5 7009AC angular contact ball bearing ships with scannable batch codes linking directly to the manufacturer’s authenticity database.
| Parameter | Value |
|---|---|
| Designation | 7006 7008CTYNSP5 7009AC |
| Bearing Type | Angular Contact Ball Bearing |
| Material | Available in Gcr15 or stainless steel variants |
| Number of Rows | Single |
| Seal or Shield Type | Zz, 2RS, Open |
| Precision Class | P0, P6, P5, P4 |
| Lubrication | Grease or Oil |
| Vibration | Z1V1, Z2V2, Z3V3, Z4V4 |
| Origin | Shandong, China |
Note: The TYN suffix in the 7008CTYNSP5 designation is an unverified cage or internal design code that requires manufacturer catalog confirmation prior to final cross-referencing.
| Industry | Typical Applications |
|---|---|
| Machine Tool Manufacturing | High-speed spindle assemblies, precision grinding headstocks |
| Precision Equipment | Robotics joint actuators, high-speed pump drive shafts |
A mismatched contact angle or overlooked precision suffix turns a routine replacement into catastrophic downtime. Procurement teams frequently source replacements based solely on the base number, ignoring the critical 15° or 25° contact angles required for specific axial load profiles. When a standard clearance bearing is forced into a high-speed spindle without accounting for thermal expansion, the inner ring expands, eliminating internal clearance and causing immediate thermal binding [NEED_CITE: rolling bearing failure mode classification per ISO 15243]. Sourcing the correct X&S 7006 7008CTYNSP5 7009AC angular contact ball bearing requires strict adherence to suffix decoding, ensuring the cage material and precision class align perfectly with the spindle’s operational envelope.
Matching the exact operational demands of machine tool spindles requires looking far beyond the basic bore and outside diameter. The X&S 7006 7008CTYNSP5 7009AC angular contact ball bearing range provides specific contact angle variants to balance radial and axial loads effectively. By verifying the exact precision class and cage design, technical buyers ensure the selected bearing withstands the intense centrifugal forces generated at high rotational speeds without compromising the machining accuracy of the finished part.
High-speed spindle environments generate substantial friction heat, directly impacting internal clearance and lubricant lifespan. If the selected bearing lacks the appropriate clearance class to compensate for thermal expansion, the rolling elements will skid, leading to rapid cage failure. Oil-air or oil-jet lubrication systems are typically required to manage these temperatures, demanding open or lightly shielded bearing configurations to allow adequate oil flow. Furthermore, any contamination from metallic wear particles in the gearbox or spindle housing will severely degrade the raceway surface, making precise seal selection or external filtration critical for maintaining operational integrity [NEED_CITE: impact of lubrication contamination on bearing fatigue life per ISO 281].
The fundamental difference between the variants in this series lies in their contact angle and precision designations. The "C" suffix denotes a 15° contact angle, optimizing the bearing for high-speed applications where radial loads dominate and minimal axial deflection is acceptable. Conversely, the "AC" suffix indicates a 25° contact angle, providing substantially higher axial rigidity for heavy-duty cutting operations. Precision classes dictate the running accuracy; while P0 is sufficient for general industrial motors, machine tool spindles demand P5 or P4 tolerances to prevent vibration and ensure superior surface finishes on machined components. Selecting the wrong precision tier introduces microscopic runout that amplifies exponentially at high RPMs.
Overlooking a single suffix character during the cross-referencing process frequently results in unplanned downtime and scrapped production batches. Installing a P0 grade bearing in a precision grinding spindle guarantees excessive vibration, ruining the surface finish of expensive workpieces and forcing premature spindle rebuilds. Similarly, ignoring the required preload arrangement or contact angle leads to uneven load distribution across the rolling elements, causing localized spalling and catastrophic raceway failure [NEED_CITE: premature bearing failure mechanisms and economic impact in manufacturing]. These hidden costs far exceed the initial savings of purchasing an incorrectly specified, cheaper alternative.
Our distribution approach focuses on rigorous technical validation rather than simple part number matching. When sourcing the 7008CTYNSP5 variant, we actively verify the specific cage material and unverified suffix codes against the manufacturer’s latest engineering catalogs to prevent field failures. We ensure that cross-referencing covers the base number, contact angle, and precision class simultaneously, eliminating the risk of installing a 15° bearing where a 25° configuration is mandated by the OEM. Every shipment includes comprehensive batch traceability, allowing maintenance teams to verify the exact production lot and original test certificates through official brand applications.
To ensure optimal spindle performance and longevity, buyers should provide detailed operational parameters, including maximum rotational speed, anticipated radial and axial loads, and the specific lubrication method utilized in the equipment. Supplying the original OEM equipment number or existing spindle drawing allows our engineering team to perform a comprehensive cross-reference check, verifying that the selected contact angle and precision class perfectly match the application requirements. This technical review prevents costly installation errors and guarantees the bearing integrates seamlessly into the existing machine tool architecture.
Q: How do you verify the authenticity of these bearings using official apps?
A: Every bearing features a unique QR code linked to the manufacturer’s database. By scanning this code with the official brand application, procurement and maintenance teams can instantly verify the production batch, original factory test results, and distribution chain. This digital traceability eliminates the risk of installing counterfeit components with soft inner rings that cause premature spindle failure under high-speed operational loads.
Q: Why must clearance, cage material, and precision suffixes be matched together?
A: Matching only the base designation ignores critical internal geometry. A bearing with the correct bore but wrong clearance will thermally bind at high speeds, while an incorrect cage material will fail under specific centrifugal forces. Aligning all suffixes ensures the bearing handles the exact thermal expansion, lubrication flow, and rotational dynamics required by precision machine tool spindles, preventing catastrophic downtime.
Q: What is the difference between 15° (C) and 25° (AC) contact angles in spindles?
A: The 15° contact angle, denoted by the "C" suffix, provides lower axial stiffness but significantly higher speed capability, making it ideal for high-RPM milling spindles. The 25° contact angle, marked as "AC", offers greater axial rigidity to withstand he*operations. Selecting the correct angle is vital for maintaining machining accuracy and preventing premature raceway fatigue.
Q: How do you select the correct precision class for machine tool spindles?
A: Standard P0 or P6 classes are suitable for general industrial motors, but machine tool spindles require P5 or P4 precision to minimize vibration and runout at high speeds. Higher precision ensures the rolling elements and raceways maintain strict geometric tolerances, which is essential for achieving superior surface finishes on machined parts and extending the operational lifespan of the entire spindle assembly.
Our engineers will respond within 12 hours with a tailored solution.
Request Quote| Bearing Type | Angular Contact Ball Bearing |
| Brand | SKF |
| Quality Standard | ISO 9001 / TS 16949 |
| Precision Grade | P0 / P5 / P6 (custom) |
| Material | Chrome Steel / Stainless |
| Cage Material | Steel / Brass / Polyamide |
| Lubrication | Grease / Oil (specify) |
| Operating Temp. | -40°C to +200°C |
| Min. Order Qty | 1 pc (samples available) |
| Prototype Lead Time | 7 Working Days |
| Load Capacity | Contact for C0/Cr values |
| Speed Rating | Contact for ndm limit |
| Vibration Level | Z1 / Z2 / Z3 (custom) |
| Noise Level | V1 / V2 / V3 (custom) |
| Fatigue Life | L10h per ISO 281 |
| Sealing Options | Open / Z / 2Z / RS / 2RS |
Our engineering team can modify bearing dimensions, materials, seals, and clearances to meet your specific operating requirements. Submit your drawing or spec sheet for a tailored proposal.
Main shaft bearings, gearbox bearings, and generator bearings for onshore and offshore wind turbines.
Heavy-duty bearings for crushers, conveyors, and rotary equipment in extreme dust and shock-load environments.
High-temperature bearings for rolling mills, continuous casting, and furnace applications.
Wheel hub bearings, transmission bearings, and e-motor bearings for passenger and commercial vehicles.
Axle box bearings, traction motor bearings, and gearbox bearings meeting EN/UIC railway standards.
High-precision spindle bearings, angular contact bearings, and super-precision bearings for CNC and robotics.
Our engineers analyze your operating conditions -- load, speed, temperature, environment -- and select or design the optimal bearing solution to maximize service life and reduce total cost of ownership.
Need non-standard dimensions, special materials, or modified clearances? We can modify standard SKF bearings or manufacture fully custom solutions with a 7-day prototype turnaround.
When bearings fail prematurely, our team conducts root-cause analysis using advanced diagnostic tools to identify the failure mode and recommend corrective action.
We deploy vibration monitoring, thermal imaging, and oil analysis programs that detect bearing deterioration early -- reducing unplanned downtime by up to 40%.
Proper installation is critical to bearing performance. Our certified technicians provide on-site installation support, alignment verification, and operator training worldwide.
From initial selection through end-of-life, our dedicated account managers provide scheduled maintenance plans, re-lubrication programs, and replacement forecasting for enterprise clients.
NDA protected · Free samples for orders > $50K · Reply within 12 hours