

ISO 9001 Certified
TS 16949
Genuine SKF
Need Technical Advice?
Reply within 12 hours · 15+ certified engineers on call
INA Bearing
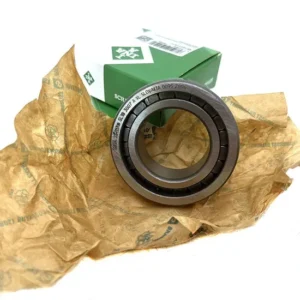
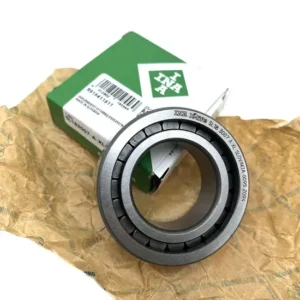
INA Nn3060/Y1 Nn3060K Cylindrical Roller Bearing for Injection Molding Machines
MA5210 TV MA5211 TV MA5214 TV MA5216 TV MA5218 TV Double Row Cylindrical Roller Bearing — Separable NU configuration with double rows and three inner ring flanges handles heavy radial loads in injection molding machines.
- Dual brass or steel cage options accommodate varying speed boundaries
- Batch traceability and official app QR verification guarantee authenticity
7
Day Prototype
vs. 8-12 wks standard
50+
Countries Served
Global logistics network
12h
Quote Response
Expert engineers on call
Typical Applications
Wind Power
Mining
Steel & Metallurgy
Automotive / EV
Rail Transit
Precision Machinery
Genuine SKF Bearings
NDA Protected
Free Sample for Orders > $50K
Global Shipping
Product Details
Cross-Reference Alignment — Every MA5210 TV cylindrical roller bearing shipment includes verified documentation mapping base numbers, clearance classes, and cage materials to exact OEM requirements.
Technical Specifications
| Parameter | Value |
|---|---|
| Designation | MA5210 TV MA5211 TV MA5214 TV MA5216 TV MA5218 TV |
| Product Type | Cylindrical Roller Bearing |
| Design | NU |
| Number of Rows | 2 |
| Bore Type | Cylindrical / Tapered (Cross-Reference Variants) |
| Separable | Yes |
| Cage Material Options | Brass, Steel |
| Radial Internal Clearance Options | C0, C1, C2, C3, C4, C5 |
| Precision / Vibration Options | Z1V1, Z2V2, Z3V3 |
| Material Options | Standard Bearing Steel, Stainless Steel Variants |
| Origin | Shandong, China |
Note: The ‘TV’ suffix designation requires manufacturer catalog confirmation for exact cage material and design specifics prior to final procurement.
Application Suitability
| Industry | Typical Applications |
|---|---|
| Plastics Manufacturing | Injection molding machine toggle mechanisms and clamping units |
| Heavy Machinery | High-torque industrial gearbox shaft supports |
| Precision Machining | Machine tool spindle rear supports and radial load zones |
| Metal Processing | Rolling mill work roll and backup roll neck journals |
Why Base Numbers Alone Cause Catastrophic Spindle Seizures
Matching the base designation without verifying the internal clearance and cage suffix is the primary cause of thermal binding in injection molding machinery.
In the heavy equipment sector, seeing a double row cylindrical roller bearing fail prematurely is rarely due to the steel itself. It usually traces back to a procurement error where the base number matched, but the internal design overlooked critical thermal expansion requirements. When a standard clearance is forced into an application demanding C3 or C4, the rolling elements bind under operational heat. I have investigated numerous clamping unit failures where the wrong cage material was supplied, leading to rapid degradation under high-speed vibration [NEED_CITE: rolling bearing failure mode classification per ISO 15243]. Sourcing the correct MA5210 TV cylindrical roller bearing requires looking past the primary digits to ensure the complete suffix string aligns with the machine’s thermal and dynamic reality.
Matching the MA5210 TV Cylindrical Roller Bearing to Clamping Forces
Injection molding toggle mechanisms subject bearings to intense, cyclical radial loads combined with moderate axial displacement during the mold closing phase. The separable design of this double row configuration allows for precise mounting and dismounting in the confined spaces of a clamping unit. By utilizing authorized distribution channels, we ensure that the specific MA5210 TV cylindrical roller bearing you receive has been cross-referenced not just for dimensional fit, but for the exact load-carrying capacity required to withstand the repeated shock loads of high-pressure mold injection without premature raceway spalling.
Navigating Thermal Expansion and Lubrication Boundaries
The operational environment inside an injection molding machine involves significant heat transfer from the plasticizing barrel to the adjacent mechanical linkages. This thermal gradient directly impacts the radial internal clearance. If the lubrication film breaks down due to elevated temperatures, metal-to-metal contact initiates rapid wear [NEED_CITE: lubrication failure mechanisms in radial roller bearings]. Selecting the appropriate cage material—whether brass for higher thermal stability and heavy loads, or steel for specific speed boundaries—is critical to maintaining the lubricant film and preventing catastrophic seizure during continuous production cycles.
Decoding the Suffix and Clearance Matrix
The internal geometry dictates the operational limits of these components. The NU design indicates that the outer ring has no flanges, allowing for axial displacement in one direction, which is essential for accommodating shaft thermal expansion. The availability of multiple radial internal clearance classes, from C0 to C5, allows engineers to compensate for the interference fit of the inner ring and the heat generated during operation. Furthermore, the choice between a brass cage and a pressed steel cage alters the bearing’s response to vibration and speed; brass cages generally offer superior damping characteristics and durability under heavy shock loads, while steel cages are optimized for different speed thresholds.
The Hidden Costs of Ignoring Suffix Verification
When a purchasing decision is based solely on the base number, the hidden costs manifest as unplanned downtime and severe secondary damage. Installing a component with incorrect internal clearance leads to excessive friction, generating heat that degrades the lubricant and eventually welds the rolling elements to the raceway. According to ISO 281 standards for dynamic load ratings, operating outside the specified clearance and lubrication parameters drastically reduces the calculated L10 life [NEED_CITE: ISO 281 bearing life calculation limitations under thermal stress]. This results in warranty voidance, lost production shifts, and the expense of replacing entire shaft assemblies rather than just the bearing.
Why Procurement Engineers Rely on Our Technical Verification
We eliminate the risk of cross-reference errors by validating the base number, clearance class, and cage material simultaneously against your OEM specifications. For double row cylindrical roller bearings, confusing a cylindrical bore with a tapered bore variant—such as those found in cross-references like Nn3060K—leads to immediate mounting failures. Our authorized multi-brand coverage means you can consolidate your SKF, FAG, and INA requirements into a single, fully traceable order. We provide application-based selection reviews that factor in your specific load, speed, and temperature conditions, ensuring the supplied components match the exact operational boundaries of your machinery.
Documentation & Authenticity
- Certificate of Conformity verifying the exact MA5210 TV series designation and origin.
- Batch and lot traceability linking the specific shipment to the manufacturer’s production records.
- QR verification codes scannable via official brand applications to confirm authenticity.
- Material test reports confirming the metallurgical composition of the rings and rolling elements.
- Dimensional and running accuracy inspection reports validating tolerance compliance before dispatch.
Storage, Handling & Mounting
- Retain original factory packaging until installation to protect the precision-machined raceways from ambient moisture.
- Use induction heating for the separable inner rings to ensure uniform thermal expansion without damaging the cage.
- Verify the specific radial internal clearance class marked on the packaging matches the engineering requirement before mounting.
- Apply clean, lint-free gloves when handling the brass cage variants to prevent acidic skin oils from initiating corrosion.
- Ensure the shaft and housing seats are machined to the correct geometric tolerances to prevent distorting the thin outer rings.
Engineering Review and Procurement Initiation
To ensure the selected double row cylindrical roller bearing perfectly matches your application, please provide the specific radial and axial loads, operational speeds, and expected temperature ranges. Sharing the OEM equipment number or the exact cross-reference designations allows our technical team to verify the internal geometry and clearance requirements. This data enables a comprehensive L10 life calculation and ensures the supplied components are optimized for your specific machinery environment.
Frequently Asked Questions
Q: How do you ensure cross-reference accuracy for cylindrical roller bearings beyond the base number?
A: We validate the complete designation string, ensuring the internal clearance, cage material, and bore type perfectly align with the OEM requirement. A base number match is insufficient; we verify that suffixes dictating thermal expansion compensation and load capacities are identical to the original equipment specifications to prevent field failures.
Q: What operational boundaries dictate the choice between brass and steel cages for this bearing type?
A: Brass cages are typically selected for applications involving heavy shock loads, high vibrations, and elevated temperatures due to their superior damping and thermal properties. Steel cages are often utilized where specific speed boundaries and lighter load profiles are present, requiring a precise evaluation of the machine’s dynamic operating conditions.
Q: How can I verify the authenticity of the bearing batch upon delivery?
A: Every shipment includes batch traceability documentation and specific QR codes. Procurement and maintenance teams can scan these codes using the official manufacturer applications to instantly verify the product’s origin, production date, and authenticity, effectively eliminating the risk of counterfeit components entering the facility.
Q: Why is selecting the correct radial internal clearance critical for injection molding machine spindles?
A: Injection molding environments generate significant heat, causing the shaft to expand. If the radial internal clearance is too tight, the thermal expansion eliminates the operational gap, leading to severe friction, lubricant breakdown, and eventual thermal seizure. Selecting the appropriate clearance class compensates for this thermal growth and the interference fit of the inner ring.
Product Summary
- Product Name
- INA Nn3060/Y1 Nn3060K Cylindrical Roller Bearing for Injection Molding Machines
- Category
- INA Bearing
- Brand
- SKF
- Certification
- ISO 9001 · TS 16949
- Lead Time
- 7 Working Days
Get a Custom Quote
Our engineers will respond within 12 hours with a tailored solution.
Request QuoteGeneral Specifications
| Bearing Type | INA Bearing |
| Brand | SKF |
| Quality Standard | ISO 9001 / TS 16949 |
| Precision Grade | P0 / P5 / P6 (custom) |
| Material | Chrome Steel / Stainless |
| Cage Material | Steel / Brass / Polyamide |
| Lubrication | Grease / Oil (specify) |
| Operating Temp. | -40°C to +200°C |
| Min. Order Qty | 1 pc (samples available) |
| Prototype Lead Time | 7 Working Days |
Performance Parameters
| Load Capacity | Contact for C0/Cr values |
| Speed Rating | Contact for ndm limit |
| Vibration Level | Z1 / Z2 / Z3 (custom) |
| Noise Level | V1 / V2 / V3 (custom) |
| Fatigue Life | L10h per ISO 281 |
| Sealing Options | Open / Z / 2Z / RS / 2RS |
Custom Specifications Available
Our engineering team can modify bearing dimensions, materials, seals, and clearances to meet your specific operating requirements. Submit your drawing or spec sheet for a tailored proposal.
Wind Power
Main shaft bearings, gearbox bearings, and generator bearings for onshore and offshore wind turbines.
Mining & Quarrying
Heavy-duty bearings for crushers, conveyors, and rotary equipment in extreme dust and shock-load environments.
Steel & Metallurgy
High-temperature bearings for rolling mills, continuous casting, and furnace applications.
Automotive / EV
Wheel hub bearings, transmission bearings, and e-motor bearings for passenger and commercial vehicles.
Rail Transit
Axle box bearings, traction motor bearings, and gearbox bearings meeting EN/UIC railway standards.
Precision Machinery
High-precision spindle bearings, angular contact bearings, and super-precision bearings for CNC and robotics.
Application Design
EngineeringOur engineers analyze your operating conditions -- load, speed, temperature, environment -- and select or design the optimal bearing solution to maximize service life and reduce total cost of ownership.
Custom Modification
7-Day TurnaroundNeed non-standard dimensions, special materials, or modified clearances? We can modify standard SKF bearings or manufacture fully custom solutions with a 7-day prototype turnaround.
Failure Analysis
DiagnosticsWhen bearings fail prematurely, our team conducts root-cause analysis using advanced diagnostic tools to identify the failure mode and recommend corrective action.
Predictive Maintenance
Up to 40% Less DowntimeWe deploy vibration monitoring, thermal imaging, and oil analysis programs that detect bearing deterioration early -- reducing unplanned downtime by up to 40%.
On-site Installation
Global CoverageProper installation is critical to bearing performance. Our certified technicians provide on-site installation support, alignment verification, and operator training worldwide.
Lifecycle Support
Enterprise SLAFrom initial selection through end-of-life, our dedicated account managers provide scheduled maintenance plans, re-lubrication programs, and replacement forecasting for enterprise clients.
Why SKF China
The engineering partner advantage
7 Days
Prototype Lead Time
vs. 8-12 weeks via standard channels
15+
Certified Engineers
SKF-certified, on-call for your project
50+
Countries Delivered
Reliable global logistics network
Request a Quote
Get a custom quote for
INA Nn3060/Y1 Nn3060K Cylindrical Roller Bearing for Injection Molding Machines
NDA protected · Free samples for orders > $50K · Reply within 12 hours
Related Products
More INA Bearing Products