ISO 9001 Certified
TS 16949
Genuine SKF
Need Technical Advice?
Reply within 12 hours · 15+ certified engineers on call
IKO Bearing
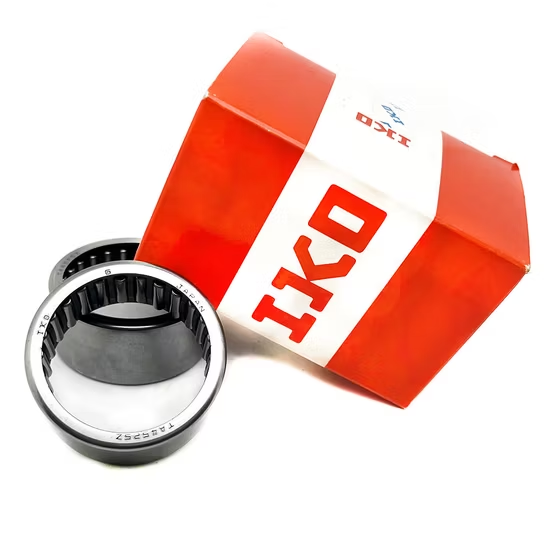
Genuine NK32/20 NK32/30 RNA49/28 RNA69/28 Needle Roller Bearing for Stamping Mould [WARN] draft identifier mismatch
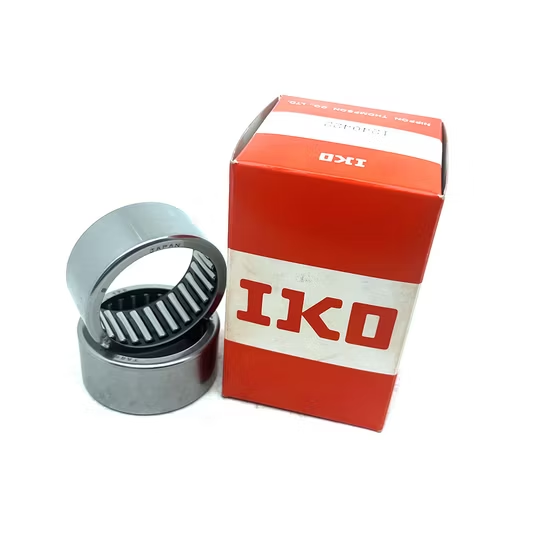
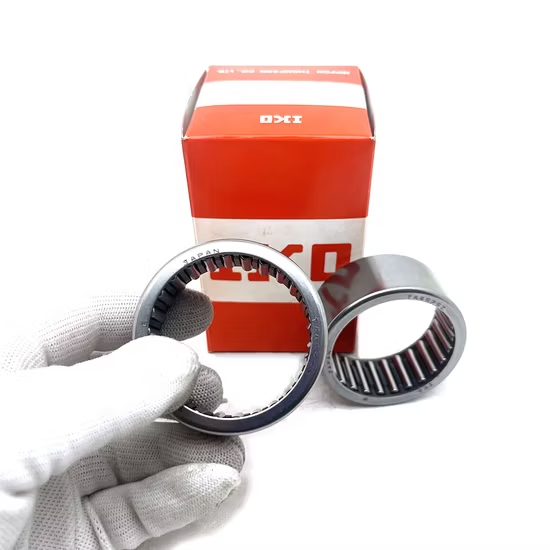
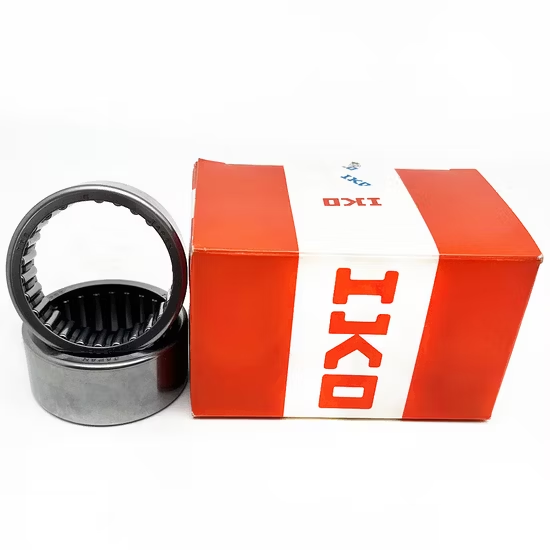
NK32/20 NK32/30 RNA49/28 RNA69/28 Needle Roller Bearings — open-type needle roller bearings in bearing steel with cage, available in P0 through P2 precision grades for stamping moulds and machine tool spindles.
- NK and RNA series: without inner ring design for compact shaft mounting
- Single and double row variants, with or without outer ring configurations
Full batch and lot traceability provided with every shipment for supply chain verification.
7
Day Prototype
vs. 8-12 wks standard
50+
Countries Served
Global logistics network
12h
Quote Response
Expert engineers on call
Typical Applications
Wind Power
Mining
Steel & Metallurgy
Automotive / EV
Rail Transit
Precision Machinery
Genuine SKF Bearings
NDA Protected
Free Sample for Orders > $50K
Global Shipping
Product Details
Verified Authenticity Scanning — Every NK32/20 NK32/30 RNA49/28 RNA69/28 needle roller bearing we dispatch carries a scannable QR code linking directly to the manufacturer’s official validation application.
Technical Specifications
| Parameter | Value |
|---|---|
| Designation | NK32/20 NK32/30 RNA49/28 RNA69/28 |
| Bearing Type | Needle Roller Bearing |
| Design Variant | With outer ring, without inner ring |
| Cage | With cage |
| Number of Rows | Single and double |
| Seal or Shield Type | Open |
| Precision Class | P0, P6, P5, P4, P2 |
| Material | Bearing steel |
| Separated | Separated |
| Origin | China |
Application Suitability
| Industry | Typical Applications |
|---|---|
| Stamping Mould | Guide pillar bushings, die cushion mechanisms, high-speed reciprocating sliding cores |
| Machine Tool Spindles | Precision rotary tables, indexing head support journals, tailstock quill assemblies |
| Industrial Gearboxes | Planetary gear shaft supports, high-torque intermediate shaft journals, compact reduction stages |
Why Stamping Dies Fail Before the Steel Yields
Internal clearance and cage material mismatches cause catastrophic binding long before the die steel reaches its fatigue limit.
When sourcing replacement components for high-speed reciprocating mechanisms, procurement teams often match the base dimension series but overlook the critical suffix details governing internal geometry. A standard clearance installed in a high-thermal-expansion environment leads to rapid thermal binding, while an incorrect cage material shatters under intense vibrational shocks [NEED_CITE: rolling bearing failure mode classification per ISO 15243]. This exact oversight once caused a cage fragmentation event in a progressive die, locking the press and destroying the entire tooling assembly. Securing the exact NK32/20 NK32/30 RNA49/28 RNA69/28 needle roller bearing configuration prevents these hidden dimensional traps.
Matching the Reciprocating Shock Environment
High-speed stamping operations subject guide components to intense, repetitive shock loads rather than smooth continuous rotation. The separated design with a rigid cage ensures the rolling elements maintain precise spacing during rapid directional reversals, preventing edge-loading and skewing. Selecting the correct NK32/20 NK32/30 RNA49/28 RNA69/28 needle roller bearing variant ensures the compact cross-section handles the extreme radial forces without compromising the tight dimensional envelope of the die shoe.
Thermal Expansion and Lubrication Demands
Frictional heat generated during continuous high-speed stamping significantly alters the internal operating clearance. An open design facilitates direct oil splash or mist lubrication, which is essential for flushing out metallic wear debris and carrying heat away from the contact zone [NEED_CITE: thermal management in high-speed rolling element bearings]. Selecting the appropriate precision class and internal clearance compensates for the thermal expansion of the shaft and housing, preventing the rolling elements from binding when the die reaches its peak operating temperature.
Decoding the NK and RNA Dimension Series
The NK and RNA prefixes denote a specific cross-sectional profile featuring an outer ring but relying on the hardened shaft itself as the inner raceway. The numerical suffixes, such as 32/20 or 49/28, dictate the precise boundary dimensions and the dimension series, which directly correlate to the load-carrying capacity and the maximum permissible shaft diameter. Understanding these specific designation codes ensures the replacement component fits the existing machined housing bore while providing the necessary radial section thickness to support the applied die tonnage.
The Downtime Cost of Suffix Neglect
Installing a component that matches the base numbers but lacks the required precision grade or cage specification results in unpredictable operational life. According to ISO 281 fatigue life calculation frameworks, even minor deviations in internal geometry or surface finish drastically reduce the dynamic load rating in oscillating applications [NEED_CITE: life calculation methods per ISO 281]. This leads to unplanned press stoppages, scrapped production batches, and expensive emergency die repairs that far exceed the initial component savings.
Why Our Technical Review Protects Your Tooling
We systematically verify the cage material, precision class, and internal clearance against your specific press tonnage and stroke rate, rather than just shipping the base number. Our cross-reference protocol ensures that when substituting brands, the internal design variant and dimensional tolerances remain perfectly aligned with the original equipment manufacturer’s requirements. Every shipment includes full batch traceability, eliminating the risk of counterfeit components with soft inner rings that fail prematurely under heavy die loads. We maintain deep inventory across all major international brands to consolidate your mixed-brand MRO requirements into a single, verified shipment.
Documentation & Authenticity
- Certificate of Conformity confirming the exact P-grade tolerance for your spindle or die application.
- Batch and lot traceability linking the specific cage assembly back to the original manufacturing run.
- Official app QR verification to instantly rule out cloned codes and counterfeit outer rings.
- Material test report validating the bearing steel metallurgy and heat treatment hardness.
- Dimensional and running accuracy inspection report verifying the open bore tolerances before dispatch.
Storage, Handling & Mounting
- Retain the original VCI packaging until installation to prevent surface corrosion on the precision-ground outer ring.
- Ensure the mating shaft journal is induction-hardened and ground to the correct roughness, as the inner ring is absent.
- Apply the recommended high-speed stamping oil immediately after mounting to protect the exposed open cage and rolling elements.
- Verify the housing bore roundness and surface finish to prevent outer ring distortion during the press-fit installation.
- Use dedicated installation sleeves to avoid damaging the separated cage assembly when driving the component into the die shoe.
Engineering Your Exact Replacement
To ensure the selected configuration survives your specific press cycle, please provide the radial load profile, stroke frequency, and operating temperature range for our L10 life review. If you are replacing an existing component, sharing the original OEM equipment number or the exact suffix markings currently on the housing allows us to perform a precise cross-reference validation. Our engineering team will then confirm the optimal clearance class and precision grade to match your die’s thermal and shock requirements.
Frequently Asked Questions
Q: Why must clearance and cage material be matched alongside the base NK or RNA number?
A: The base number only defines the boundary dimensions. In high-speed stamping, thermal expansion requires specific internal clearances to prevent binding, while heavy shock loads demand a cage material that resists fragmentation. Ignoring these suffix details leads to rapid thermal seizure or catastrophic cage failure, destroying the entire die assembly despite the outer dimensions fitting perfectly.
Q: What are the shaft hardness requirements when using these NK and RNA series bearings?
A: Because the NK and RNA series operate without an inner ring, the shaft itself acts as the inner raceway. The mating journal must be induction-hardened to an appropriate depth and precision-ground to a specific surface roughness. If the shaft is too soft or rough, it will cause rapid wear on the rolling elements and lead to premature spalling and catastrophic die failure.
Q: How should open-type bearings be lubricated in a stamping mould application?
A: The open design lacks integrated seals, making it ideal for the continuous oil splash or mist lubrication systems typically used in high-speed presses. This external lubrication method not only reduces friction at high reciprocating speeds but also continuously flushes away metallic wear debris generated by the sliding die components, significantly extending the operational life of the bearing.
Q: How do the P0 through P2 precision classes affect machine tool spindle performance?
A: Higher precision classes like P4 or P2 enforce much stricter tolerances on the outer ring bore, radial runout, and dimensional accuracy. In machine tool spindles, utilizing these tighter grades minimizes vibration and rotational runout, ensuring superior surface finish on the machined parts and preventing uneven load distribution that causes premature fatigue in high-speed rotary applications.
Product Summary
- Product Name
- Genuine NK32/20 NK32/30 RNA49/28 RNA69/28 Needle Roller Bearing for Stamping Mould [WARN] draft identifier mismatch
- Category
- IKO Bearing
- Brand
- SKF
- Certification
- ISO 9001 · TS 16949
- Lead Time
- 7 Working Days
Get a Custom Quote
Our engineers will respond within 12 hours with a tailored solution.
Request QuoteGeneral Specifications
| Bearing Type | IKO Bearing |
| Brand | SKF |
| Quality Standard | ISO 9001 / TS 16949 |
| Precision Grade | P0 / P5 / P6 (custom) |
| Material | Chrome Steel / Stainless |
| Cage Material | Steel / Brass / Polyamide |
| Lubrication | Grease / Oil (specify) |
| Operating Temp. | -40°C to +200°C |
| Min. Order Qty | 1 pc (samples available) |
| Prototype Lead Time | 7 Working Days |
Performance Parameters
| Load Capacity | Contact for C0/Cr values |
| Speed Rating | Contact for ndm limit |
| Vibration Level | Z1 / Z2 / Z3 (custom) |
| Noise Level | V1 / V2 / V3 (custom) |
| Fatigue Life | L10h per ISO 281 |
| Sealing Options | Open / Z / 2Z / RS / 2RS |
Custom Specifications Available
Our engineering team can modify bearing dimensions, materials, seals, and clearances to meet your specific operating requirements. Submit your drawing or spec sheet for a tailored proposal.
Wind Power
Main shaft bearings, gearbox bearings, and generator bearings for onshore and offshore wind turbines.
Mining & Quarrying
Heavy-duty bearings for crushers, conveyors, and rotary equipment in extreme dust and shock-load environments.
Steel & Metallurgy
High-temperature bearings for rolling mills, continuous casting, and furnace applications.
Automotive / EV
Wheel hub bearings, transmission bearings, and e-motor bearings for passenger and commercial vehicles.
Rail Transit
Axle box bearings, traction motor bearings, and gearbox bearings meeting EN/UIC railway standards.
Precision Machinery
High-precision spindle bearings, angular contact bearings, and super-precision bearings for CNC and robotics.
Application Design
EngineeringOur engineers analyze your operating conditions -- load, speed, temperature, environment -- and select or design the optimal bearing solution to maximize service life and reduce total cost of ownership.
Custom Modification
7-Day TurnaroundNeed non-standard dimensions, special materials, or modified clearances? We can modify standard SKF bearings or manufacture fully custom solutions with a 7-day prototype turnaround.
Failure Analysis
DiagnosticsWhen bearings fail prematurely, our team conducts root-cause analysis using advanced diagnostic tools to identify the failure mode and recommend corrective action.
Predictive Maintenance
Up to 40% Less DowntimeWe deploy vibration monitoring, thermal imaging, and oil analysis programs that detect bearing deterioration early -- reducing unplanned downtime by up to 40%.
On-site Installation
Global CoverageProper installation is critical to bearing performance. Our certified technicians provide on-site installation support, alignment verification, and operator training worldwide.
Lifecycle Support
Enterprise SLAFrom initial selection through end-of-life, our dedicated account managers provide scheduled maintenance plans, re-lubrication programs, and replacement forecasting for enterprise clients.
Why SKF China
The engineering partner advantage
7 Days
Prototype Lead Time
vs. 8-12 weeks via standard channels
15+
Certified Engineers
SKF-certified, on-call for your project
50+
Countries Delivered
Reliable global logistics network
Request a Quote
Get a custom quote for
Genuine NK32/20 NK32/30 RNA49/28 RNA69/28 Needle Roller Bearing for Stamping Mould [WARN] draft identifier mismatch
NDA protected · Free samples for orders > $50K · Reply within 12 hours
Related Products
More IKO Bearing Products